Reducing Repositioning in Large-Part Machining
In large-part machining, a workpiece often needs to go through multiple machining steps before it is completed. Because different machining areas may have different accessibility, machining directions, and process requirements, the workpiece may need to be re-clamped or repositioned during the machining process.
Repositioning does not necessarily mean that the machining plan is problematic. However, every additional adjustment of the workpiece position adds another step that needs to be controlled within the production process. In addition to the time required for re-clamping, confirming the positioning reference, interrupting the machining process, and coordinating different operations can also affect the overall workflow.
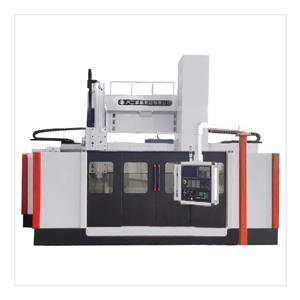
Therefore, for large parts, reducing unnecessary workpiece repositioning is not simply about making clamping faster. It requires looking at the entire machining process and determining which positioning operations are necessary and which can be reduced through a more appropriate CNC Large Vertical Lathe machining plan.
1. Why Are Large Parts More Likely to Require Repositioning?
Large parts often have relatively large dimensions and more complex machining requirements. The same workpiece may need to be machined in several different areas. When the current workholding setup cannot provide access to the next area that needs to be machined, the workpiece may need to be repositioned.
For large parts, however, the size, shape, and distribution of machining areas can make the process more complicated when planning the machining process for a CNC Large Vertical Lathe.
Therefore, repositioning is usually not caused by a single factor. It is related to the workpiece structure, machining areas, and overall process planning.
If these factors are not considered early enough when planning the machining process, actual production may involve frequent re-clamping, re-alignment, or transfers of the workpiece between different machines.
2. Repositioning Adds More Than Just Clamping Time
When a workpiece needs to be repositioned, the most obvious impact is the additional time required for clamping and adjustment. For large parts, however, the effects of repositioning often go beyond this.
· First, every new setup requires the position of the workpiece to be checked again. The operator needs to make sure that the workpiece is in the correct machining position and establish or confirm the positioning relationship required for the current operation.
· Second, when different machining areas on the same workpiece have a relationship that needs to be maintained, repositioning introduces another step that needs to be controlled during the machining process. Each time the workpiece changes position, the subsequent machining operations need to be checked to ensure that they can continue as intended.
· Repositioning can also interrupt an otherwise continuous machining process. If a workpiece has to be repeatedly transferred between different machines, the production process becomes divided into more independent stages. In addition to actual machining time, lifting, transferring, repositioning, and rechecking also become part of the overall production process.
Therefore, when evaluating the impact of repositioning, it is not enough to look at how long a single setup takes. It is more important to consider how many additional steps repositioning introduces into the entire machining workflow.
3. Rethinking the Machining Plan to Reduce Repositioning
Reducing repositioning does not mean that every large part must be completely machined in a single setup. For some complex workpieces, multiple setups are a reasonable part of the machining process.
A more practical approach is to determine before finalizing the machining plan:
Which operations require repositioning, and which operations can continue in the current setup?
This needs to be evaluated based on the actual machining range of the CNC Large Vertical Lathe, the machining areas of the workpiece, and the overall process arrangement.
For example, during equipment selection and process planning, the main machining areas of the workpiece can first be identified. The next step is to determine whether the machining range of the selected equipment can cover these areas. If certain operations must be transferred to another machine, it is then worth considering whether this transfer is necessary and how it will affect the overall production process.
It is also important to consider how the workpiece will be stably supported and positioned during machining. For large parts, physically moving the workpiece may itself involve additional operations. Therefore, reducing unnecessary position adjustments can help make the machining process more continuous.
The goal is not simply to pursue “fewer setups,” but to create a more appropriate relationship between workpiece positioning, machining range, and process planning.
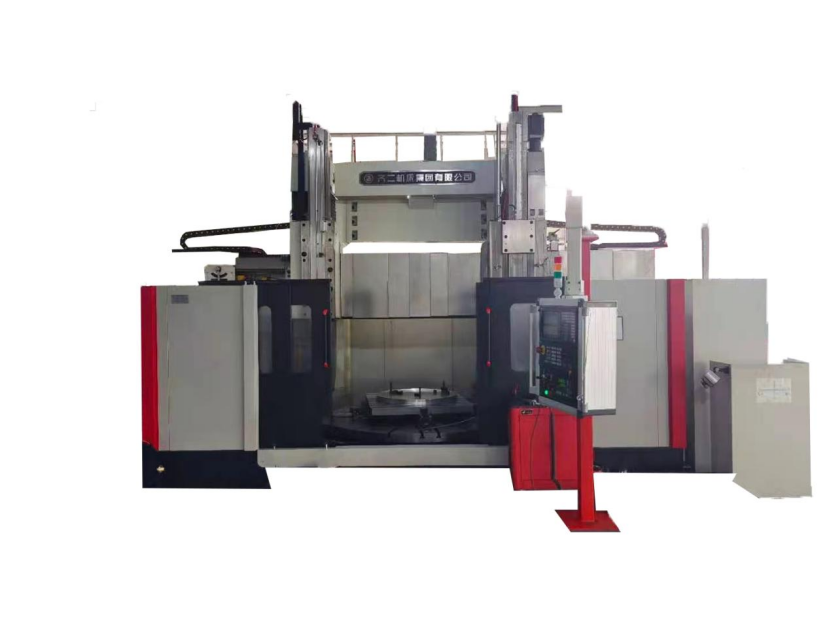
4. Which Large-Part Machining Situations Require More Attention to Repositioning?
Not every machining task needs to treat repositioning as a major concern. Buyers and process engineers can assess this issue based on their actual production conditions.
If a workpiece has any of the following characteristics, repositioning is worth considering carefully during equipment and process planning:
·The same workpiece requires machining in several different areas;
·The main machining areas are located in different directions;
·The machining range of the current equipment cannot easily cover all required areas;
·The workpiece needs to be repositioned frequently during machining;
·The workpiece needs to be transferred between different machines multiple times;
·Repositioning significantly increases clamping, alignment, or process coordination time.
For this type of production task, CNC Large Vertical Lathe selection should not focus only on one machining parameter. Instead, the entire process should be considered, from the moment the workpiece enters the machine until machining is completed.
Consider the case of wind turbine main bearings. These parts necessitate machining of the inner and outer raceways that requires high precision for dimensions and smooth surface quality. In intermittent machining of large forged steel workpieces, variations in cutting forces may result in vibrations and tool wear. Long machining operations generate heat which in turn may affect the dimension stability.
This can help buyers avoid focusing only on the machining capability of an individual machine while overlooking the actual production process that the equipment will become part of.
Conclusion
For large-part machining, repositioning is an easily overlooked but very real part of the production process.
Consider the case of wind turbine main bearings. These parts necessitate machining of the inner and outer raceways that requires high precision for dimensions and smooth surface quality. In intermittent machining of large forged steel workpieces, variations in cutting forces may result in vibrations and tool wear. Long machining operations generate heat which in turn may affect the dimension stability.
When planning a large-part machining process or purchasing new CNC equipment such as a CNC Large Vertical Lathe, considering these factors in advance can make it easier to identify a machine configuration that fits the actual production workflow.
If you are planning a CNC machining solution for large parts, feel free to contact us to discuss a suitable equipment solution based on your actual workpieces and machining requirements.